The Duravant family of operating companies serve the food processing, packaging and material handling segments.







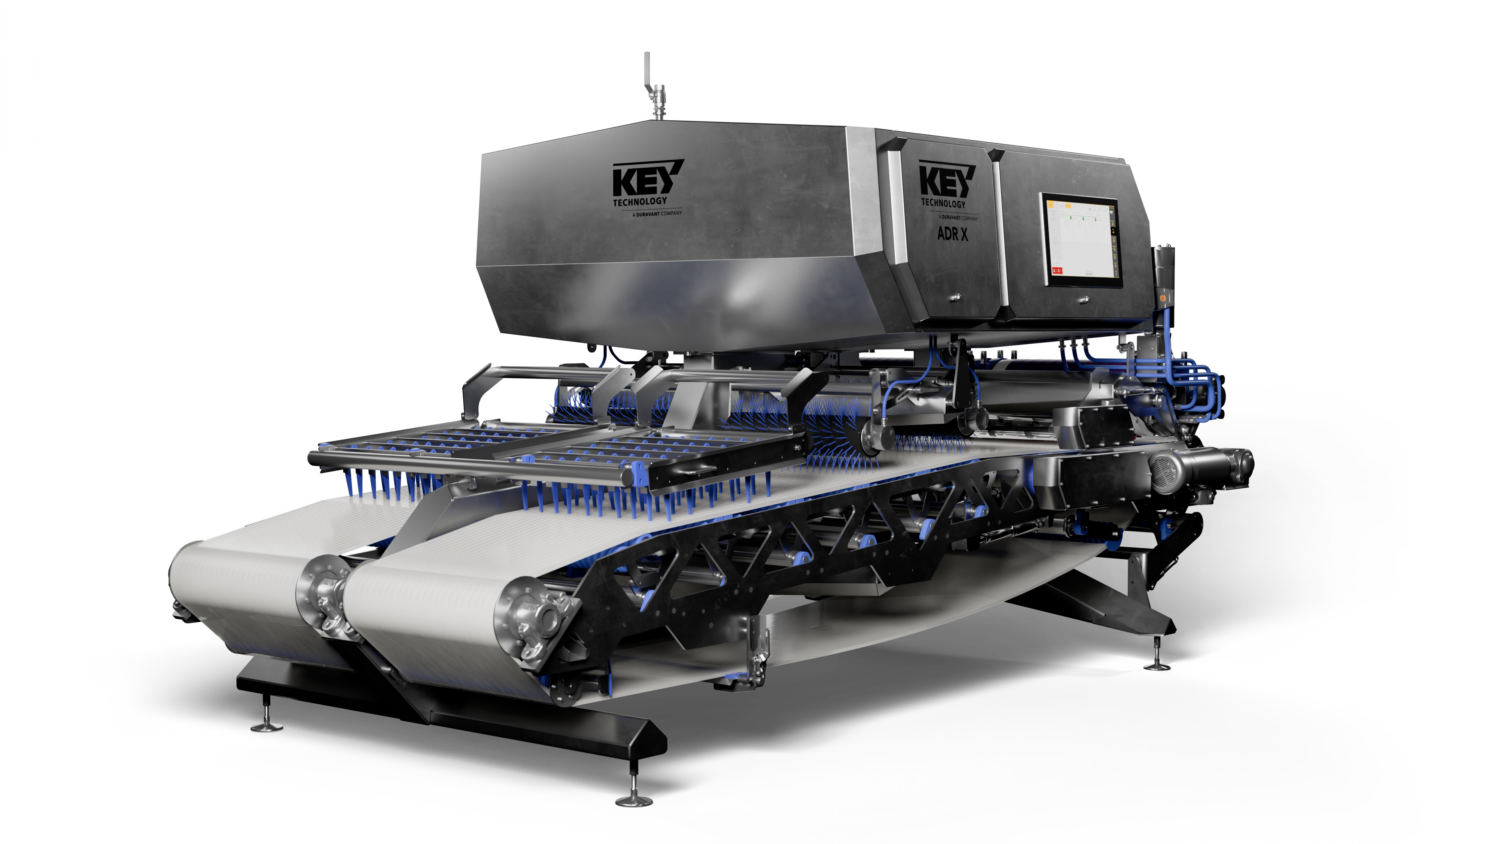
Introducing ADR X
Next-generation Automatic Defect Removal system that maximizes potato strip yield and quality with unmatched precision, hygiene and performance — backed by over 40 years of proven expertise.

Introducing COMPASS
COMPASS optical sorters take food sorting automation in a new direction by combining leading edge inspection technology with simple, intuitive operation.

Duravant Lifecycle Services
Our commitment to long-term optimized equipment performance and customer success.

A Global Leader in Food Processing Automation
Key Technology is a sorting machine manufacturer committed to being the ultimate partner of choice in optical sorting and food handling solutions.

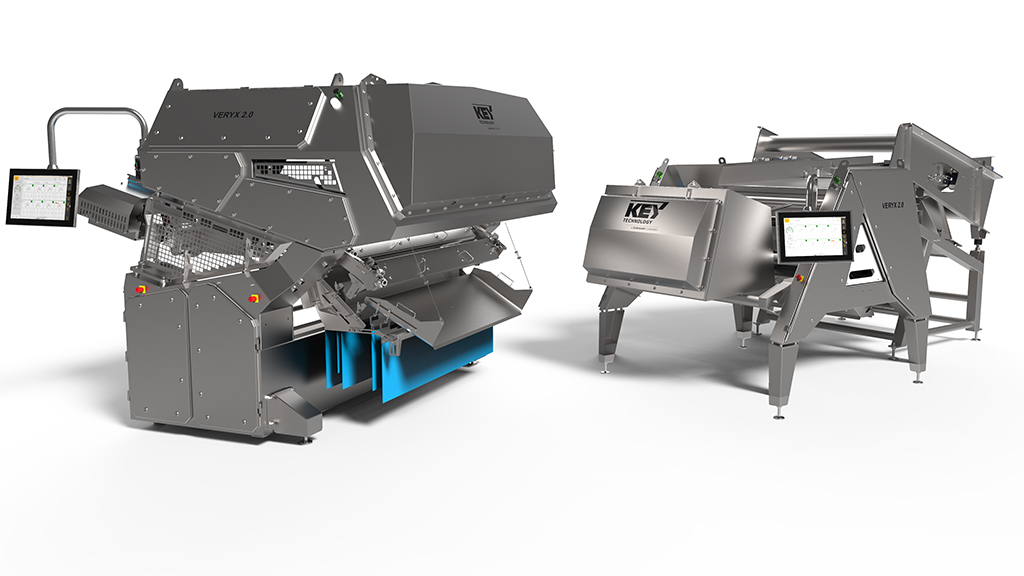
VERYX 2.0
The VERYX platform is the most powerful optical sorter for automatically managing the selection of processed and fresh foods.

Introducing Zephyr
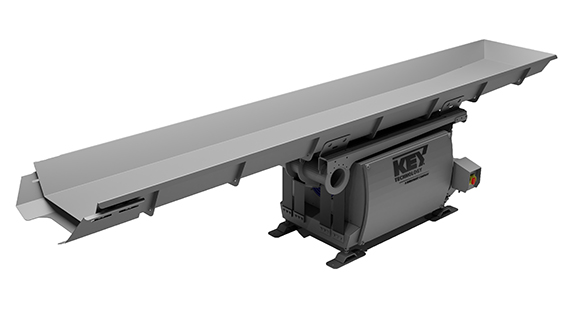
Designed for food processors who want gentle handling, the Zephyr offers reduced maintenance and a higher throughput for high capacity applications.

Live Equipment Demonstrations
Whether in-person or online, the systems you’re considering will be demonstrated and tested based on your exact requirements, with your product.

Food Processing Equipment & Sorting Machine Manufacturer
Discover the latest conveying, processing and sorting solutions from an innovative, leading global food processing equipment manufacturer. Our integrated solutions and turnkey systems comprise multiple pieces of equipment and deliver premium performance and economic value.
Industry Specialized Food Processing Solutions
Key Technology helps companies improve profitability with equipment that helps them meet their quality management objectives by maximizing the production process and reducing costs. Cost reduction includes decreasing or eliminating the need for human labor to perform certain functions on the production line.


We Drive Value for Our Customers
Key Technology is a leading global food processing equipment manufacturer. Applying unmatched processing knowledge and application expertise, Key helps customers worldwide improve quality, increase yield and reduce cost. With over 75 years of experience as a food machinery supplier, we serve dozens of industries including fruit, vegetable, nuts, potato, candy, snacks and more.
Unlike other food processing machinery suppliers or sorting machine manufacturers, Key Technology offers sorting, conveying and other processing equipment, meaning you benefit from a seamlessly integrated, customized solution from ONE source.
The world’s food processors choose Key:


Clear Vision. Clear Progress.
Key Technology’s cutting-edge optical sorting and conveying solutions set the standards for maximizing yield, efficiency and profitability. At the same time, they deliver data-driven intelligence to continually optimize and improve your operations.

Duravant Lifecycle Services
Our program is more than an investment in protecting an equipment purchase. We create a partnership that enables us to provide support throughout the entire lifecycle of our products.

News

PPM Technologies and Key Technology Introduce New Fully-Integrated Potato Chip Processing Line
May 19, 2026
Upcoming Events
Coming Soon.
At Key Technology, we understand that every operation in the food and beverage industry is unique, and our solutions have been created to reflect that. We work closely with each customer to learn about their facility layout, throughput goals, and quality standards, then configure equipment accordingly. From conveyor sizing to sorting parameters, our systems are always completely customized to make sure you get the right food processing equipment for your company’s needs.
Integration with your existing infrastructure is absolutely possible. At Key Technology, while we do specialize in delivering complete processing lines, our individual sorting, conveying, and processing units can work alongside equipment you already have in place. Our team will assess your current setup and recommend the most practical and cost-effective path forward.
Many of our systems are highly versatile because we know that in the food processing industry, production needs change with seasons, contracts, and market demand. Depending on the model and configuration, our equipment can be adjusted to handle a variety of products across categories like potatoes, vegetables, nuts, fruit, dairy, poultry, and more. Our team can help you determine which platform best fits your range of products.
Timelines are going to vary based on the complexity of the system and your existing infrastructure, but minimizing disruption to your food production is always our priority, no matter what. Our project teams plan installations around your schedule, and in many cases, phased rollouts can reduce the impact on your ongoing operations. We’ll provide a detailed implementation plan specific to your facility during the sales process.
Food processing equipment is only as effective as the people running it. Producing high-quality food products consistently requires well-trained teams, so we provide comprehensive training for both operators and maintenance staff at your facility. Through our Duravant Lifecycle Services program, we support your team beyond installation — helping you maintain production efficiency, stay aligned with food safety regulations, manage energy consumption, and get the most out of your equipment throughout its full lifecycle. We’re a long-term partner invested in your success across the food industry.